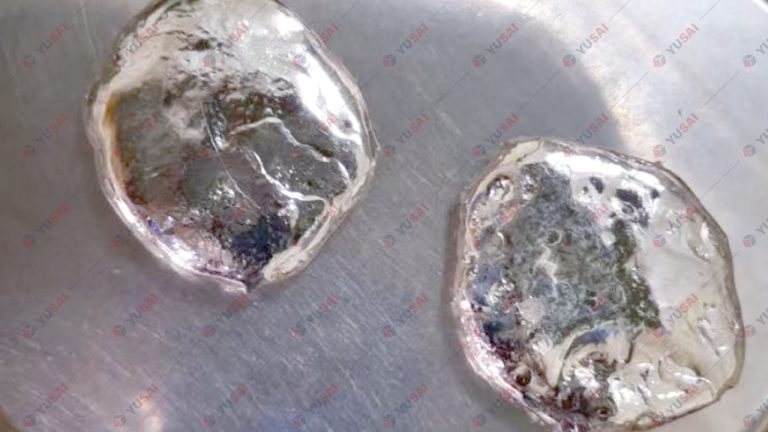
Silver is widely used in catalyst manufacturing for chemical industry. After service life expires, silver-bearing spent catalysts become an important secondary resource for silver recycling. Traditional silver recovery processes from spent catalysts include pyrometallurgical smelting, conventional electrolytic refining, ammonia leaching-reduction and single-stage nitric acid leaching & electrolysis. These methods generally suffer from high energy consumption, low silver recovery rate, severe acid mist corrosion, large amounts of waste liquid and waste residue, complicated post-treatment, unstable silver quality and high operating cost.
This paper introduces an efficient and closed-loop cyclone electrowinning process to recover silver from silver-containing spent catalysts. The whole process adopts two-stage cyclone electrowinning with precise filtration, realizing high-purity silver powder production, high silver recovery and acid liquor recycling, which is environmentally friendly and suitable for industrial continuous production.
Process Principle
Cyclone electrowinning relies on the difference in deposition potential of metal ions. High-speed circulating electrolyte eliminates concentration polarization during electrolysis, so silver ions can preferentially deposit on the cathode to form metallic silver powder. Compared with conventional electrolysis cells, cyclone electrowinning powder tank effectively suppresses redissolution of deposited silver and improves current efficiency and product quality.
Process Flow
- Nitric Acid Leaching Silver-containing spent catalyst raw material is leached with concentrated nitric acid to prepare silver nitrate solution. The pH of leachate is controlled within 2.5–3.5.
- Ceramic Membrane Precision Filtration The obtained silver nitrate solution passes through ceramic membrane filtration to remove solid impurities. Filter residue is returned to the leaching tank for re-leaching to reduce silver loss. The clear filtrate is transferred to the storage tank for electrowinning.
- First-Stage Cyclone Electrowinning The filtrate is pumped into the first-stage circulation tank connected with cyclone electrowinning units. Silver ions are reduced and precipitated as silver powder. Operating parameters:
- Initial Ag⁺ concentration: 90–120 g/L, reduced to 50–60 g/L
- Current density: 600–800 A/m²
- Electrolyte flow velocity: 6000–10000 L/hr
- Solution circulation rate: 350–450 L/h Precipitated silver powder is flushed and collected into the silver powder filter tank by circulating solution.
- pH Adjustment & Second-Stage Cyclone Electrowinning The electrolyte after first-stage electrowinning is adjusted with caustic soda to pH 2.5–2.8 and sent to the second-stage cyclone electrowinning. Operating parameters:
- Ag⁺ concentration: 50–60 g/L, reduced to 20–30 g/L
- Current density: 500–600 A/m²
- Electrolyte flow velocity: 6000–10000 L/hr
- Solution circulation rate: 350–450 L/h Silver powder generated in the second stage is also collected into the silver powder filter tank.
- Electrolyte Circulation Reuse After two-stage electrowinning, the waste electrolyte has pH 0.1–0.5. It is recycled back to the leaching procedure as nitric acid lixiviant to realize closed circulation of acid solution.
- Silver Powder Washing, Drying and Ingot Casting Collected silver powder is transferred to settling filter tank, washed with pure water at room temperature for 2–3 times until the supernatant pH reaches 6.5–7.5 to remove residual acid, nitrate and sodium ions. After washing and drying, silver powder is melted and cast into silver ingots.
Technical Advantages
✅ High silver purity and high recovery: The final silver product reaches 99.99% grade, total silver recovery rate ≥98.8%. ✅ Closed-loop solution circulation: Leaching acid is recycled, no large discharge of wastewater and hazardous gas. ✅ Low equipment corrosion: Greatly reduces acid mist compared with traditional electrolysis. No extra anode mud treatment procedure. ✅ Compact and modular design: Cyclone electrowinning units are easy to assemble, disassemble and relocate. High current density improves production capacity and cuts operating cost. ✅ Stable product quality: Precision filtration removes solid impurities before electrowinning, avoiding impurity contamination of silver powder.
Test Result
In the laboratory test, 2366.8 g silver spent catalyst was leached by diluted nitric acid under heating and stirring for 3 hours. After ceramic membrane filtration, qualified silver nitrate solution was sent for two-stage cyclone electrowinning. First-stage electrowinning ran for 1 h and produced 68.46 g bright silver powder. Second-stage electrowinning ran for 1.5 h and produced 45.84 g bright silver powder. Assay test confirms the silver product purity of 99.99%.
Application Scenarios
This technology is applicable for silver recovery from Al₂O₃ / SiO₂ supported silver catalysts, silver nitrate solution purification and secondary silver resource regeneration. It is an ideal clean metallurgy solution for precious metal recycling plants and catalyst manufacturers.